

Double deep racking is a high-density pallet storage system designed to store two pallets deep in each rack position.Compared with conventional selective pallet racking,it reduces the number of operating aisles and makes better use of available warehouse space.
This system is suitable for warehouses that need higher storage density while maintaining access to different product groups.
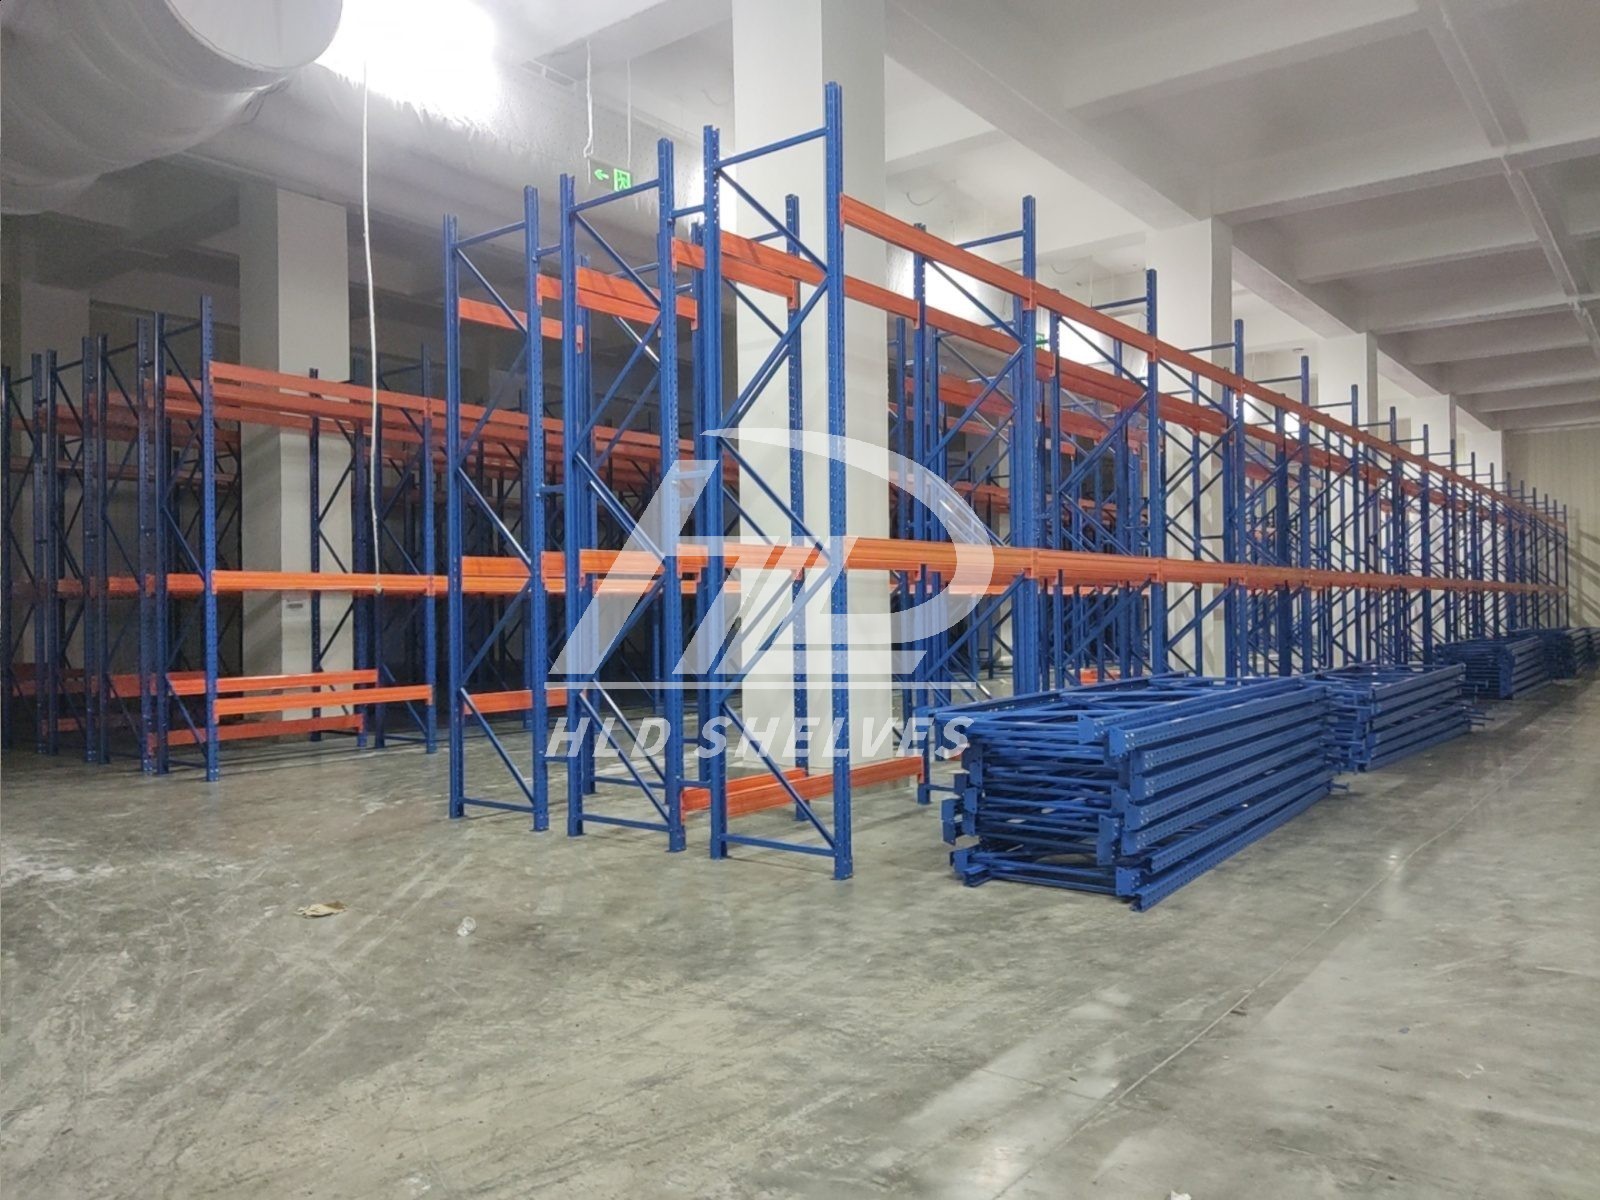
How Does Double Deep Racking Work?
Double deep racking uses two rows of pallet positions placed one behind the other.Forklifts equipped with telescopic forks or suitable reach mechanisms can access the rear pallets.
The system generally follows the Last In,First Out(LIFO)principle,as the front pallet needs to be removed before the rear pallet can be accessed.
Key Advantages of Double Deep Racking
Higher Storage Density:Stores more pallets within the same warehouse area by reducing aisle requirements.
Better Space Utilization:Makes more effective use of available floor space.
Cost-Effective Storage:Offers a balance between storage density and investment compared with some automated systems.
Flexible Configuration:Rack height,depth and load capacity can be customized according to warehouse requirements.
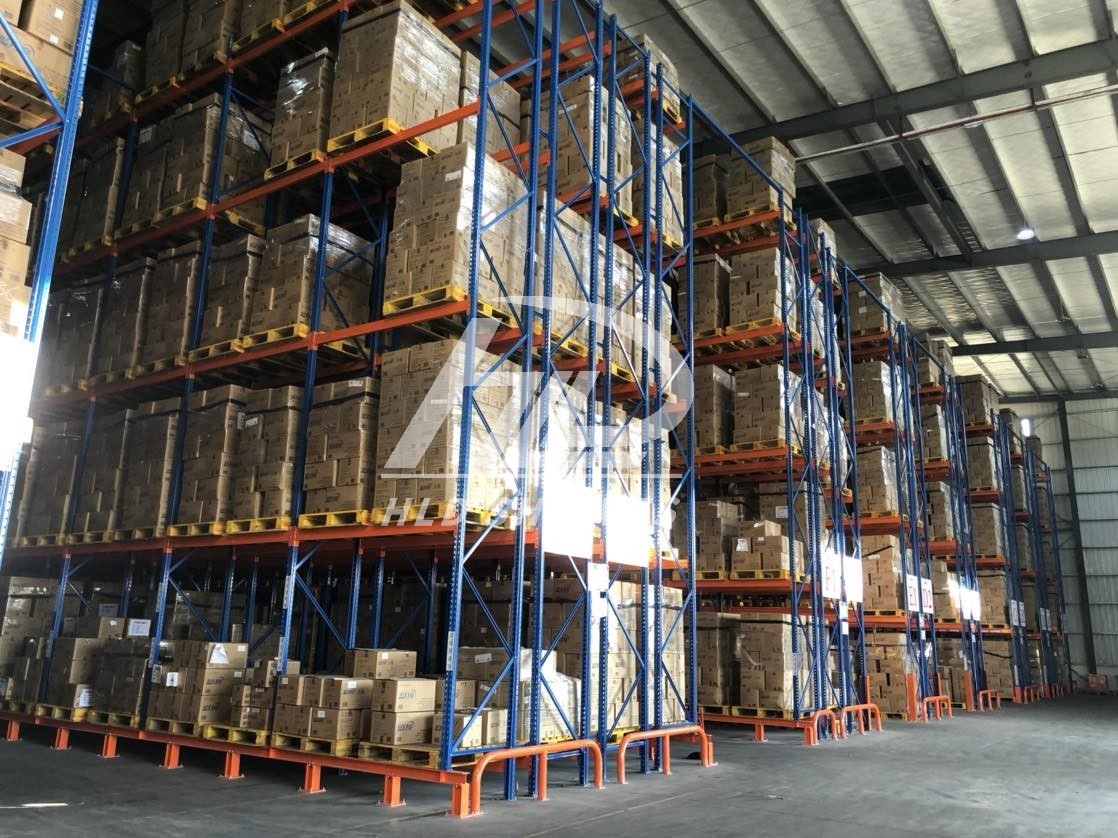
What Should You Consider Before Choosing Double Deep Racking?
Pallet dimensions,load weight,SKU quantities and inventory turnover should all be considered.Forklift compatibility is also important,as standard forklifts may not be suitable for accessing the rear pallet positions.
Double Deep Racking Manufacturer–HLD Shelves

HLD Shelves specializes in industrial pallet racking and high-density storage systems.We provide customized double deep racking solutions based on warehouse dimensions,pallet specifications and material handling requirements.
Contact HLD Shelves to discuss your warehouse layout and storage needs.
